



 acebook
 (bottom of page)

djarossens
Member
- Messages
- 42
- Location
- Switzerland
Hello,
I have been messing around with different instruments to get practice with brazing, soldering and generally working with brass and seem to have ended up with a few tenor horns, flugelhorns, trumpets and larger (alto/euphonium sizes). several are missing the lead pipe (and mouthpiece receiver) so I got to thinking about tube bending and missed a sale of an H55 from Ferrees in the UK (H55 Heavy Duty Tubing Bending Fixture). As its heavy and I'm fed up of the import duties and shipping charges I decided I'd try and make one.
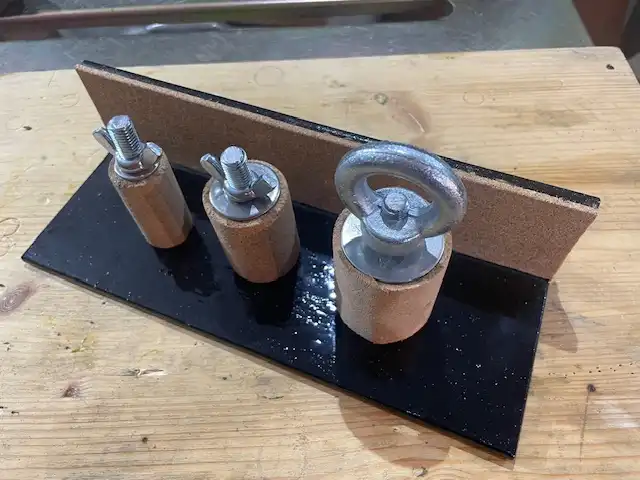
In the image you can see how far I have got.
So as I understand it the next step would be to drill holes in the base plate to allow me to fix the forms whilst bending.
On the photo from Ferrees of the tool there are many holes and I doubt these are randomly placed though I don't see a logic.
Does any one have one or could send me a scale drawing of the placement of the holes please?
Failing that what would be your ideas for how to place the holes?
Thanks for the suggestions!
I have been messing around with different instruments to get practice with brazing, soldering and generally working with brass and seem to have ended up with a few tenor horns, flugelhorns, trumpets and larger (alto/euphonium sizes). several are missing the lead pipe (and mouthpiece receiver) so I got to thinking about tube bending and missed a sale of an H55 from Ferrees in the UK (H55 Heavy Duty Tubing Bending Fixture). As its heavy and I'm fed up of the import duties and shipping charges I decided I'd try and make one.
In the image you can see how far I have got.
So as I understand it the next step would be to drill holes in the base plate to allow me to fix the forms whilst bending.
On the photo from Ferrees of the tool there are many holes and I doubt these are randomly placed though I don't see a logic.
Does any one have one or could send me a scale drawing of the placement of the holes please?
Failing that what would be your ideas for how to place the holes?
Thanks for the suggestions!


