Tech/maintenance MKvi Octave Mechanism Bent

PiccoloPirate

Senior Member
Messages
1,207
Location
South Florida
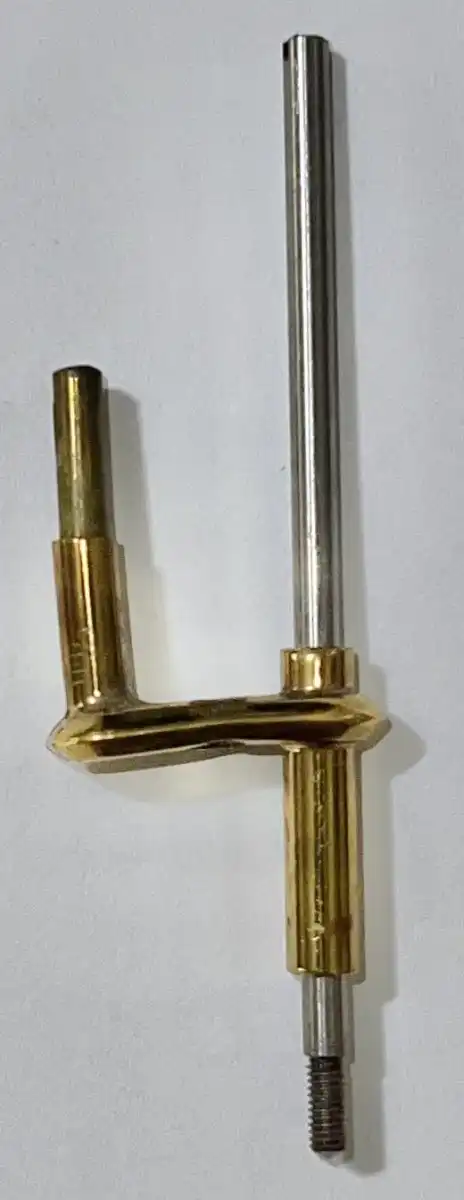
Pic of '73 Alto's bent octave mechanism part.
What is the proper way that this is repaired by a competent tech?

Thanks,
PP
FullSizeRender.jpeg
 
I'm not a tech but I wonder what you seek in a specific answer.
Depending on the tools at the techs disposal I'd think there may be more than one way to do this before it's considered the wrong way.
Also pretty sure that its soft enough for straightening the bar with appropriate leverage force in some purpose made pliars without heat or further damage is achievable and the same for the round pin which would typically have a sleeve on top anyway.
 
^^^^
Thanks.
I just straightened the upper pin
(red area), that is covered by a gray plastic sleeve when on the horn, so it is square to the wider lower pin.
Pic is before it was straightened.

For the lower bent part, that attaches to the tube, a steel flat bar, blue area, then press the top down to make it flat, as it should be. Might need a shim in white area.
There is a hole in the bent part as well.
Pic just to show general idea not final placement.

I can machine what's needed, have bar stock etc etc, and have lotsa tools, but my concern is to not fracture that part.
Was curious if it would be wise to heat it a bit first and how a tech would apply the heat.

Funny story about letting your teenage children not use their own horns. :verysad

FullSizeRender.jpeg
 
Last edited:
I would just squeeze it with parallel jaw pliers. Squeeze on the hole, so it is supported. Maybe put some thin cardboard or cork on the jaws, like from a business card.

If you just grab the end and bend, without supporting the area where the hole is (which is why it’s bent there) You risk having that metal distort or tear, which would be harder to fix.
 
^^^^
Thanks,
I tried that with the 5" Groblet smooth jaw parallel pliers, but the jaws are only .250" wide. The lower concave surface needs a stout metal bar along its entire length.
Picture shows what I'll make/try unless anyone sees a fault in this idea.
Used a piece of wood to show idea.

Mill a bevel (yellow area) on a 5/16" or 3/8" piece of square metal bar stock.
Put a thin 1/8" wide shim between the metal bar and end area (red dot) and try a .020" thick shim to start, then thicker if necessary. This will increase the space to allow for the bending.
Use a small C clamp (blue areas) and turn it as necessary to straighten.
Care taken to avoid bending the tube.

Will try it later as house/lawn chores and bread baking first.
May an uplifting Gospel prayer, on Picc, before turning the clamp.
And a Guinness for courage. :thumb:

IMG_2933.jpeg
 
Last edited:
Made what was necessary and the horn works, with the neck in the correct position, for me, once again.
Using the old HR 95/0/M Berg and have a Bronze 100/0/M on the way. Hopefully it measures accurately, as is made right.
 
Last edited:
^^^^
Thanks,
I tried that with the 5" Groblet smooth jaw parallel pliers, but the jaws are only .250" wide. The lower concave surface needs a stout metal bar along its entire length.
Picture shows what I'll make/try unless anyone sees a fault in this idea.
Used a piece of wood to show idea.

Mill a bevel (yellow area) on a 5/16" or 3/8" piece of square metal bar stock.
Put a thin 1/8" wide shim between the metal bar and end area (red dot) and try a .020" thick shim to start, then thicker if necessary. This will increase the space to allow for the bending.
Use a small C clamp (blue areas) and turn it as necessary to straighten.
Care taken to avoid bending the tube.
That's pretty much how it's done. Support the underside of the key arm, apply pressure to the top.
What I tend to do is drill a hole in a block of Delrin that's a snug fit for the barrel, pop the barrel into the hole, stick the rod screw down it (to help stiffen the barrel) then use a press to straighten out the key arm. This method helps to keep the arm perpendicular to the barrel.
Just take it nice and slowly.

You might not get it perfectly straight (it'll be good enough) because you often have to take the metal past the point at which its flat and let it spring back - and the easiest way to do that is the grind/sand a little relief in the block around the centre point of the bend.
 
Picture of 3/8" square stock, beveled and .035" shim glued on, to allow for bending.
Used as in picture in post #6.
Señor Howard's method is much better, elegant and with a touch of class, ask Barrie & Cahn.
Outfitted Barrie's 72' Hatteras long ago.
Salon was a Fabergé Disco dance floor, with lights and music.
Fun times.

IMG_2963.jpeg
 
Last edited:

Social

New! Social Feeds

Look out for the navigation icon:

Follow CafeSaxophone

Latest Song of the Month

Trending

Forum statistics

Topics
32,064
Messages
578,455
Members
8,130
Latest member
tommyliehe
Back
Top Bottom